Design a 3D Printed Cookie Cutter That Actually Cuts
By Moopky ·
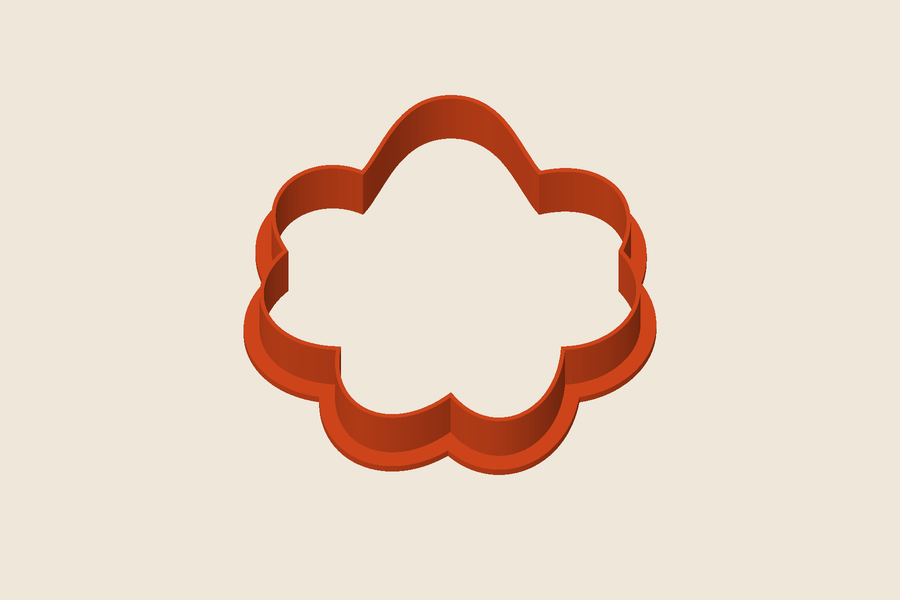
A cutter needs a shape that can be produced as a continuous wall, enough depth for the material being shaped and a grip that lets pressure reach the edge. A detailed illustration is not automatically a good cutting outline. Begin with a simple silhouette and inspect the geometry at its intended size. The cookie cutter maker creates a digital model; it does not certify a printed tool for food contact or guarantee cutting performance.
The flower illustration is a render of our own engine output. No physical cutting test or food-contact assessment is implied. Use a non-food craft material to examine shape and handling while developing the design. A commercial food-use workflow requires a suitable food-safe process and an assessment of the finished object, not just a successful STL export.
Make the exterior silhouette do the work
Choose an outline that remains recognizable without internal shading or thin decorative marks. Broad curves and clear corners are easier to inspect than many tiny points. The tool uses the largest exterior contour, so a source containing several separate illustrations can produce an unexpected selection. Prepare one dominant silhouette per export. Remove unrelated logos, frames and registration marks from the source copy.
For SVG input, use filled paths and simplify unsupported content in a vector editor. For an image, use a high-contrast silhouette and adjust the threshold until the exterior matches your intention. Inspect small gaps around the edges: an isolated pixel or a low-contrast connection can change the traced contour. If the outline looks noisy, clean the source rather than trying to repair every irregularity through dimensions alone.
Choose size from the narrowest section
Start with a 70 mm target size as a manageable experiment, then look at the narrowest necks and tightest inward corners. Two designs with the same overall width can have very different practical limits. A narrow projection may bend, snag or leave too little room to release the shaped material. Increasing the whole design can help, but it can also exceed your intended serving or craft dimensions.
The generator warns about challenging concave features, but a warning is only a prompt to inspect. It cannot predict how a particular dough, clay or other material will behave. Smooth overly sharp corners in the original drawing and compare the result. Keep enough character to identify the design while removing details that would be difficult to print or clean. Test those decisions with the actual intended process.
Balance the wall and the flange
The default cutting wall is 0.8 mm thick and 15 mm high, with a 3 mm flange width and 2 mm flange thickness. Treat these as model starting points. Compare wall thickness with the extrusion paths in your slicer; a nominal wall can produce a different number of deposited lines depending on the profile. Check the whole perimeter, including tight corners and curves, rather than one straight segment.
The wider flange provides a broader area for handling and pressure. Inspect its placement in the preview and orient the object deliberately in the slicer. Do not assume the first imported orientation is the best printing orientation. A taller wall creates more clearance but can also be more flexible. A thicker wall can be sturdier but may change the cut. Evaluate those tradeoffs with a small trial rather than maximizing every slider.
Understand the optional stamp
The optional separate stamp is based on an inset outline. It does not reproduce arbitrary internal line art from a drawing, and it is not a full illustration-to-embossing system. If your design depends on detailed eyes, lettering or internal decorations, confirm that the generated stamp actually contains them before promising that result. The preview is the place to check the geometry, not a marketing illustration.
When the stamp is enabled, inspect both pieces and their relative sizes. They are separate objects and need deliberate arrangement on the print bed. Check that an inward offset has not erased a small feature or created an impractical narrow region. For non-food craft use, test pressing and release with a sample of the material. Keep craft tools separate from anything intended for food contact.
Review sliced paths before printing
Export the model and examine every layer in the slicer. Look for a continuous wall, a connected flange and missing segments around sharp corners. If the slicer drops a narrow feature, change the design or physical size before printing. A watertight mesh is helpful, but it does not guarantee that every wall becomes a useful extrusion path. Mesh validity and process suitability are separate checks.
Use a profile appropriate for the chosen material and printer. Check adhesion, cooling and the first-layer footprint. After a non-food trial, examine the edge for rough spots, gaps and weak areas. Do not use sanding or an unverified coating as an automatic route to food safety. Any finishing material and process need their own suitability assessment, including how the finished surface will be cleaned and maintained.
Treat food contact as its own design problem
PLA layer lines and surface defects can harbour bacteria. A spool being described as food-safe does not establish that the printer, nozzle, colourants, handling, finished surface or cleaning method produce a safe utensil. The tool makes no food-safety claim. Obtain guidance appropriate to your application and use a suitable food-safe process; when that cannot be established, use a purpose-made food-contact tool instead.
Think about repeated use as well as the first cut. Heat, washing, abrasion and storage can change a printed object’s surface and shape. Do not assume it is dishwasher-safe or suitable for a commercial kitchen. Keep documentation for the materials and process if making items for sale. Commercial permission under a software licence does not replace product-safety or food-contact requirements for the physical item.
Keep the final decision tied to evidence
Retain the source silhouette, exported dimensions and slicer profile so changes can be compared. If a test fails to release cleanly, identify whether the issue is a narrow contour, wall depth, surface condition or the material being shaped. Change one variable at a time. A cleaner silhouette may solve more than a thicker wall, while a safer application may call for an entirely different manufacturing process.
For source preparation, read why SVG conversion fails. For a solid decorative emblem rather than a cutting wall, use SVG to STL. Review the model licence before selling physical prints. Keep the distinction clear throughout the project: the generator supplies editable dimensions and downloadable geometry, while you assess the finished object’s performance, rights and suitability for its intended use.